
Goldilocks guide to inbound and outbound potato sorting: how Potato inbound and outbound sorting production line, Potato Conveyor BSSJ8-08 and Potato selection platform fit together, which operating points to set first, and what our engineers confirm before we prepare a line proposal.
In practice: Goldilocks guide to inbound and outbound potato sorting: how Potato inbound and outbound sorting production line, Potato Conveyor BSSJ8-08 and Potato selection platform fit together, which operating points to set first, and what our engineers confirm before we prepare a line proposal.
How we configure: inbound and outbound potato sorting
At Goldilocks, we configure inbound and outbound potato sorting around the hand-offs that control product quality and uptime. Potato inbound and outbound sorting production line, Potato Conveyor BSSJ8-08 and Potato selection platform cover complementary steps; the practical choice is how they share flow, access and operator attention.
Start with crop condition, the hourly target and the quality decision the line must support. We select the first machine around that operating point. Place receiving, cleaning, inspection, storage and packing in a sequence that leaves room for service access, safe transfer and clear operator sightlines.
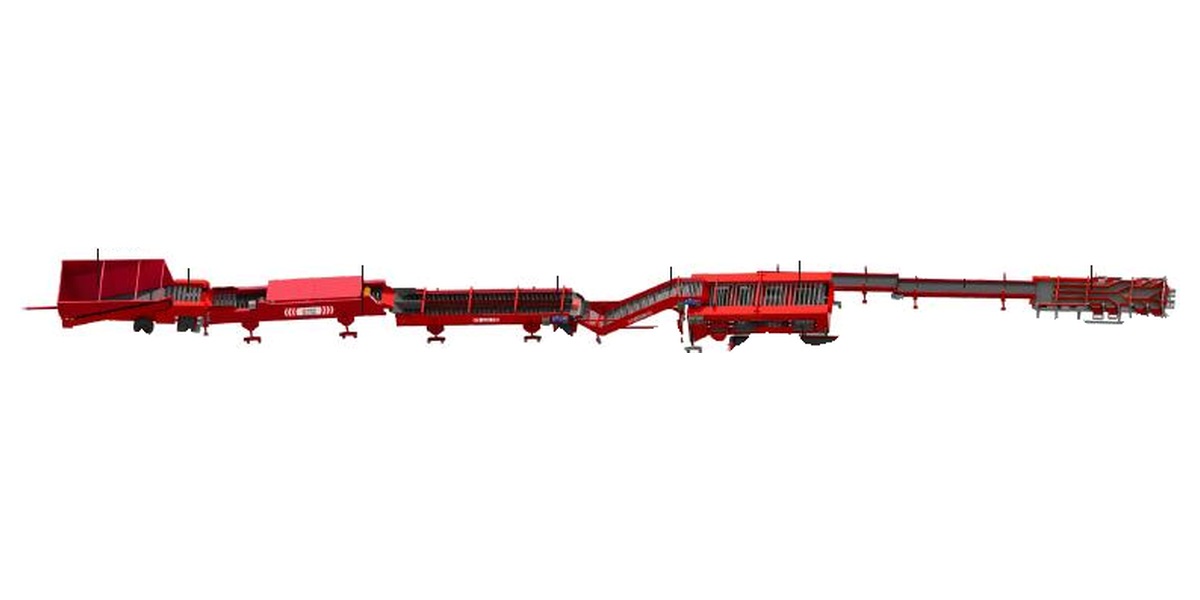
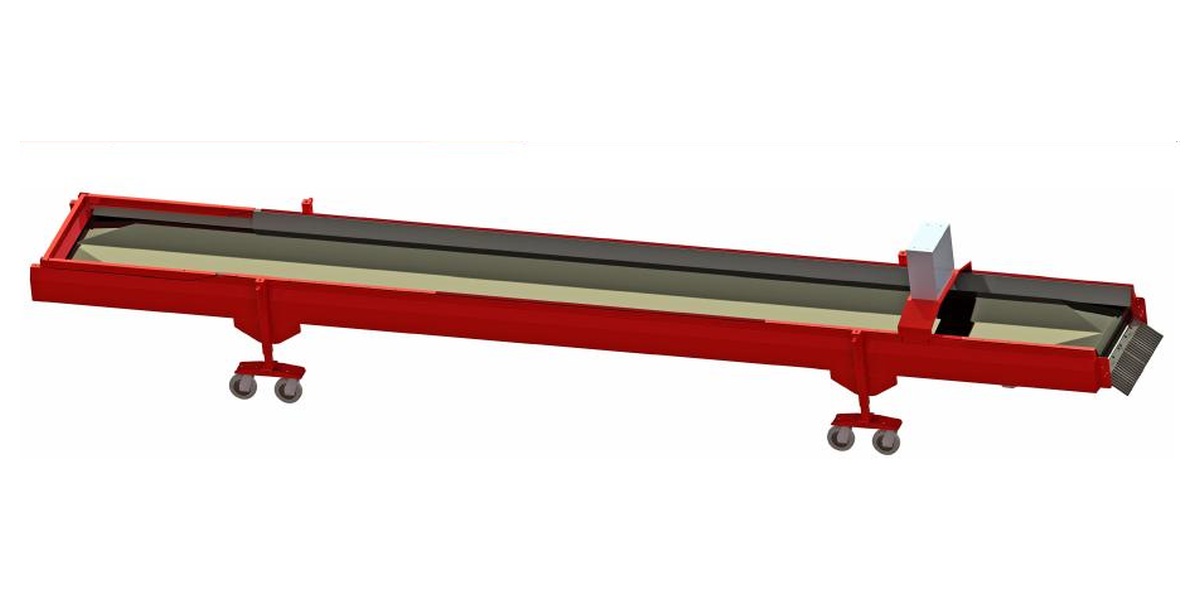
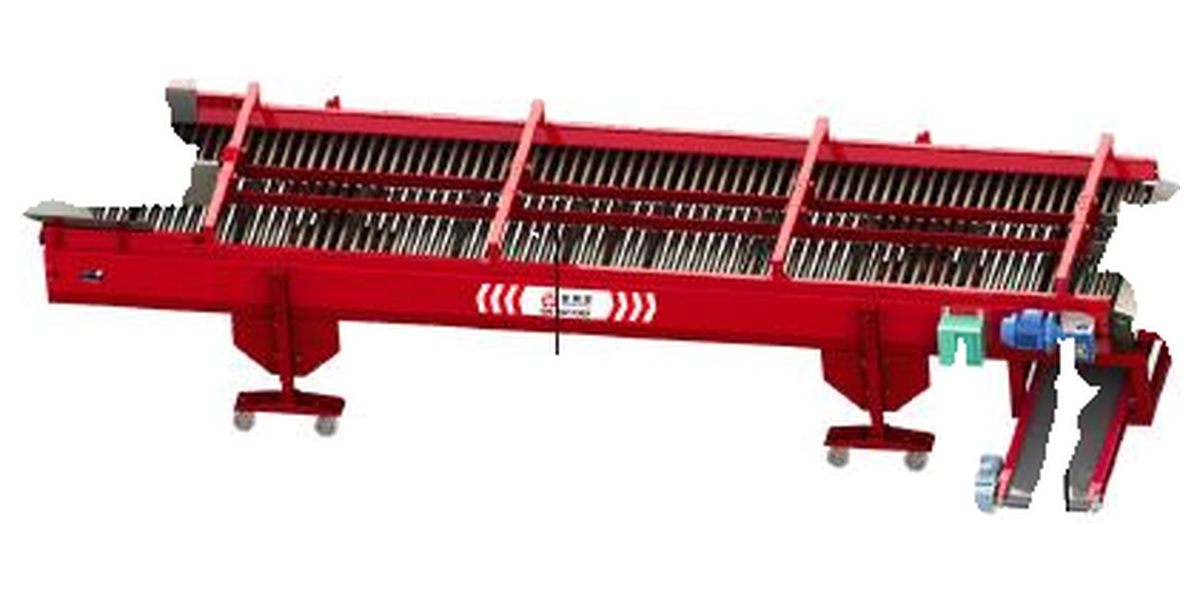
Equipment used in this line
These are the models we normally review for this process. Capacity and dimensions set the first layout; our engineers then tune the line to the crop, target flow and site.
| Model | Capacity | Dimensions | Role |
|---|---|---|---|
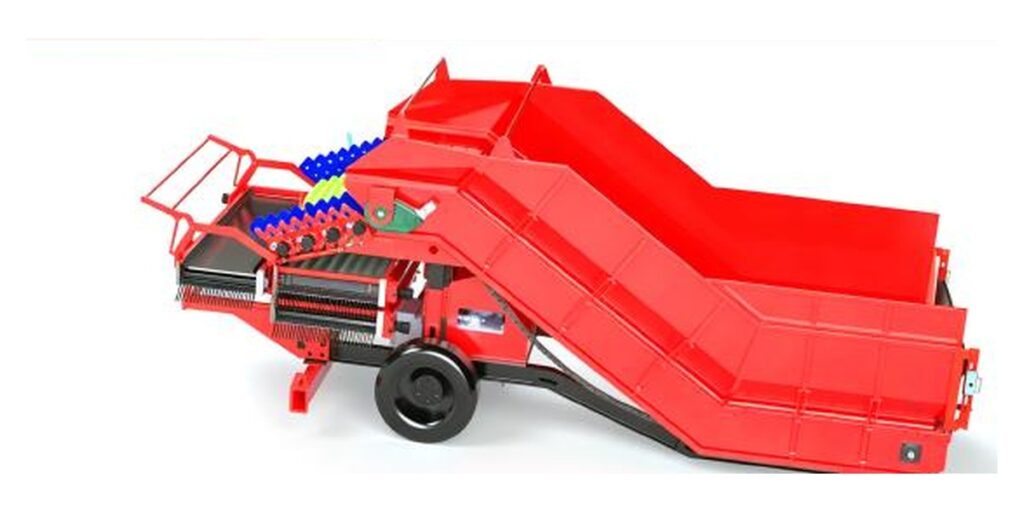
| Integrated line solution | Configured to project requirements | Water-wash line approximately 45 m | Inbound sorting; outbound sorting; cleaning; grading; packing |
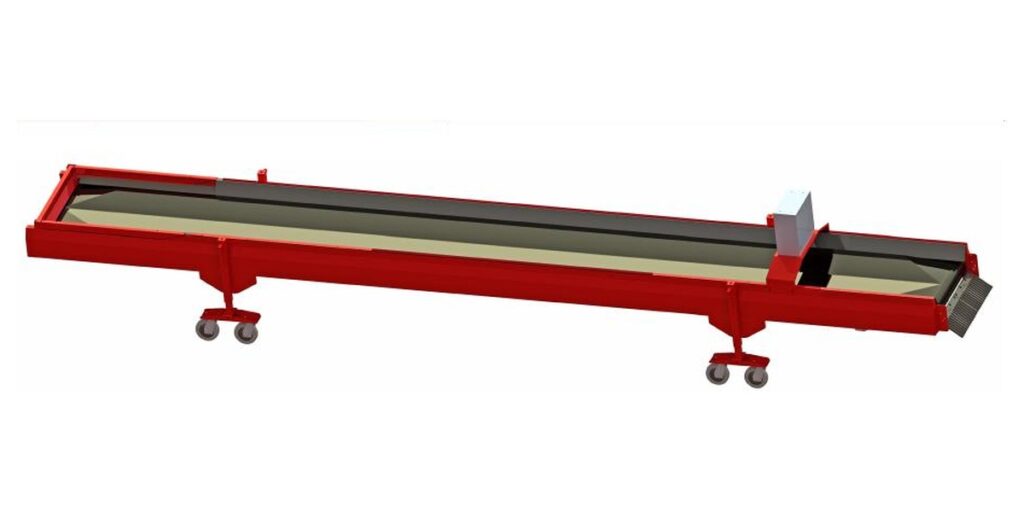
| BSSJ8-08 | Approximately 80 t/h | 8050 × 1300 × 1300 mm; belt width 800 mm; inlet height 800 mm; outlet height 490-890 mm | Conveying between cleaning, grading, storage and packing equipment |
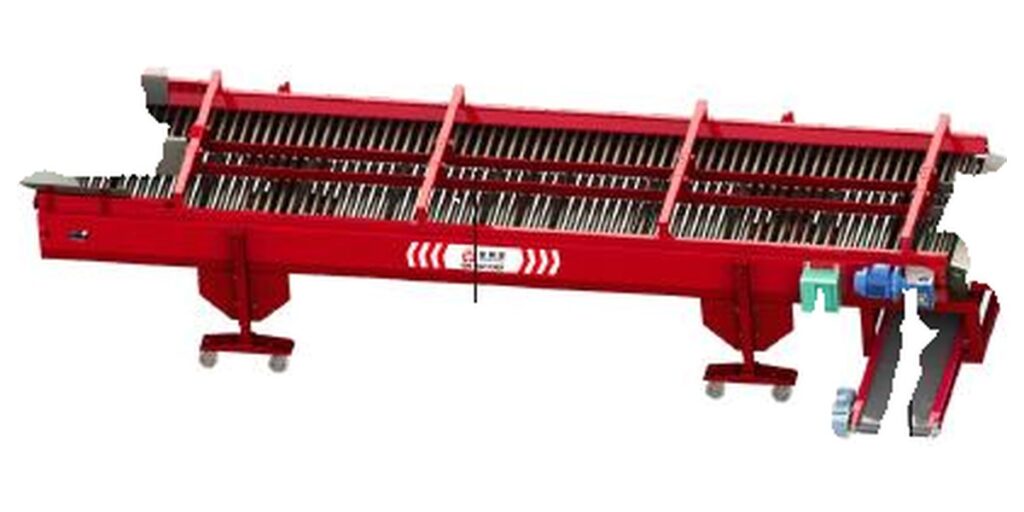
| Selection platform | 5-15 t/h | 5600 × 2150 × 1100 mm; adjustable height 960-1300 mm | Manual potato inspection before grading and packing |
How to plan the line
1. Start with the crop and flow
Start with crop condition, the hourly target and the quality decision the line must support. We select the first machine around that operating point.
2. Set the physical sequence
Place receiving, cleaning, inspection, storage and packing in a sequence that leaves room for service access, safe transfer and clear operator sightlines.
3. Prepare the project brief
Before we issue a final proposal, we confirm voltage, material condition, shift pattern, local safety requirements and the acceptance test for the installed line.
Typical bottlenecks and our method
Inbound and outbound sorting share equipment only when the traffic rules are explicit. The inbound/outbound line and BSSJ8-08 conveyor can be reviewed as a common spine, while the selection platform provides a human or quality checkpoint. Separate receiving and shipping windows, discharge directions and buffer ownership should be drawn before deciding whether one route can safely serve both flows.
Most line problems start at a transfer: one machine is rated above the next module, wet produce carries soil into inspection, or a reject stream returns to the main flow. We solve this by sizing the hand-off, buffer and discharge together.
Our usual method is a controlled material trial. We set the feed rate, check drop height and belt or roller speed, tune variable-frequency drives where fitted, then record good and reject streams at each step.
Depending on the line, the technical review can include buffer volume, belt speed, roller gap, drop height, optical lighting, near-infrared detection, pneumatic reject response and acceptance sampling.
- material condition and size range
- target flow by hour and by shift
- available footprint and service access
- power, voltage and discharge direction
- the test method used to accept the line
What we confirm before production
A reliable line starts with a clear project brief. We confirm the feedstock, moisture, size range, contamination, installation site and acceptance criteria before fixing the final arrangement or operating target.
Goldilocks configures each line after reviewing the crop, target throughput, layout, power and acceptance test. The product links above show the equipment used in this guide; contact us for a project-specific arrangement.
Tell our Goldilocks engineering team about your crop, target flow and site.
- Integrated line solution: Configured to project requirements; Water-wash line approximately 45 m; Inbound sorting; outbound sorting; cleaning; grading; packing
- BSSJ8-08: Approximately 80 t/h; 8050 × 1300 × 1300 mm; belt width 800 mm; inlet height 800 mm; outlet height 490-890 mm; Conveying between cleaning, grading, storage and packing equipment
- Selection platform: 5-15 t/h; 5600 × 2150 × 1100 mm; adjustable height 960-1300 mm; Manual potato inspection before grading and packing
Frequently asked questions
Which machine should come first for inbound and outbound potato sorting?
Start with the machine that handles the first control point in the material flow. We then size the following transfer and buffer around the same operating target.
Can the listed capacity be used as the final line capacity?
Use it as the starting point for the layout. Final throughput depends on crop condition, feed rate, size distribution, settings and the agreed acceptance test.
What do you need for a quotation?
Send the material, target flow, voltage, dimensions, service access, discharge direction, safety requirements and preferred acceptance method.
Engineering note
Goldilocks configures each line after reviewing the crop, target throughput, layout, power and acceptance test. The product links above show the equipment used in this guide; contact us for a project-specific arrangement.


 English
 Chinese
 Spanish
 German
 French
 Russian
 Urdu
 Bengali
 Kazakh
 Ukrainian
 Dutch
 Polish